

Sandblasting & Coating
Blast cleaning to the grade your specification calls out — brush-off through white metal — with coating applied to your system and the inspection records to prove it. The same building that cut and welded your part is the one that finishes it.
The Coating Is Part of the Job, Not a Handoff
A finished weldment that leaves the shop to get blasted somewhere else picks up a second freight bill, a second schedule, and a second company's idea of what your specification meant. It also picks up handling damage, and nobody owns it.
We blast and coat in house, as the last operation on the same job number. Your part goes from the welding bay to surface prep to coating without leaving the property, and the prep grade, profile, and film thickness are recorded against that job before it ships.
That matters most when the coating is specified rather than assumed — when a print calls out a near-white blast and a dry film thickness range, and somebody has to demonstrate it was actually achieved.

Blast Cleaning to a Stated Grade
Two methods on site, chosen by part size and the prep the specification calls for.
Prep Grades
- Brush-off through white metal — blast to the grade your print calls out
- Profile verified with replica tape, not estimated
- Grade and profile recorded against the job
- Full standards list below
Large Parts
- Two 1,000 lb capacity blast pots
- High-volume portable air, 375 CFM
- Weldments, bedplates, skids, tanks, and structural assemblies
- Part size limited by what our 45-ton yard crane can pick — not by a booth door
Small Parts & Finishing
- Coyote 48 airless wheel table blast
- Abrasive recycling with integral dust collection
- Consistent finish on production quantities of smaller parts
- Timesaver Speedbelt TOP 18 sanding and polishing, 18" belt
Surface Preparation Standards
Tell us the grade your specification calls out and we blast to it. The grades below are the same process at different durations — the difference is dwell time and abrasive, not equipment.
| Standard | Grade | What may remain on the surface |
|---|---|---|
| SSPC-SP 5 / NACE No. 1 | White metal blast | Nothing. No staining anywhere on the surface. Specified for immersion service and tank linings. |
| SSPC-SP 10 / NACE No. 2 | Near-white blast | Light staining on no more than 5% of each unit area. The most commonly specified grade in industrial work. |
| SSPC-SP 6 / NACE No. 3 | Commercial blast | Staining on no more than 33% of each unit area, visible only as discolouration. |
| SSPC-SP 14 / NACE No. 8 | Industrial blast | Between brush-off and commercial. Loose material removed; some tightly adherent coating may remain. |
| SSPC-SP 7 / NACE No. 4 | Brush-off blast | Tightly adherent mill scale, rust and coating may remain. Loose material removed. |
| SSPC-SP 1 | Solvent cleaning | Removes oil, grease and soluble contaminants. Normally specified ahead of any grade above. |
| SSPC-SP 11 | Power tool cleaning to bare metal | Bare metal with a minimum 1 mil profile, no staining permitted. For repair and touch-up where a pot and nozzle cannot reach. |
| SSPC-SP 15 | Commercial grade power tool cleaning | Bare metal with a minimum 1 mil profile, random staining to 33% permitted. |
| SSPC-SP 2 / SP 3 | Hand and power tool cleaning | Loose material removed with hand tools or powered brushes, discs and needle guns. No profile produced. Used for touch-up and weld-burn cleanup. |
SSPC and NACE merged into AMPP in 2021. The joint SSPC / NACE designations above remain the ones written into project specifications and are the ones we work to. Grade is verified against SSPC-VIS 1 and the profile measured with replica tape.
Inspected on Calibrated Instruments, and Recorded
Plenty of shops blast and paint. Fewer can hand you the numbers afterward. Every instrument below is NIST-traceable and calibrated on a twelve-month interval by outside laboratories accredited to ISO 17025, logged by gauge ID with its last calibration and next due date under our ISO 9001:2015 quality system.
Blast Profile
Testex replica tape with dial thickness gauges — the anchor pattern is measured against what the coating system requires, not eyeballed.
Dry Film Thickness
DeFelsko PosiTest FM and Elektro-Physik MikroTest FM5 ferrous coating thickness gauges, read after coating and recorded.
Dew Point
DeFelsko PosiTector DPM with probe. Ambient conditions are checked before the gun is picked up, because a coating applied over the dew point fails whatever the film build says.
Surface Temperature
KTA 914 and 941 and Fluke 62 infrared thermometers, confirming steel temperature is inside the coating manufacturer's window.
Applied to Your Specification
Coating systems are specified job by job. Tell us the system, the film build, and the prep grade your print requires, and we will confirm what we can apply in house before you release the order — rather than discovering it at the end.
- Airless spray application with agitating pressure pots
- Primer, finish coat, or both, to the specified system
- Prep grade, profile, dew point, and film thickness documented
- Masked and protected machined faces, bores, and bolt patterns
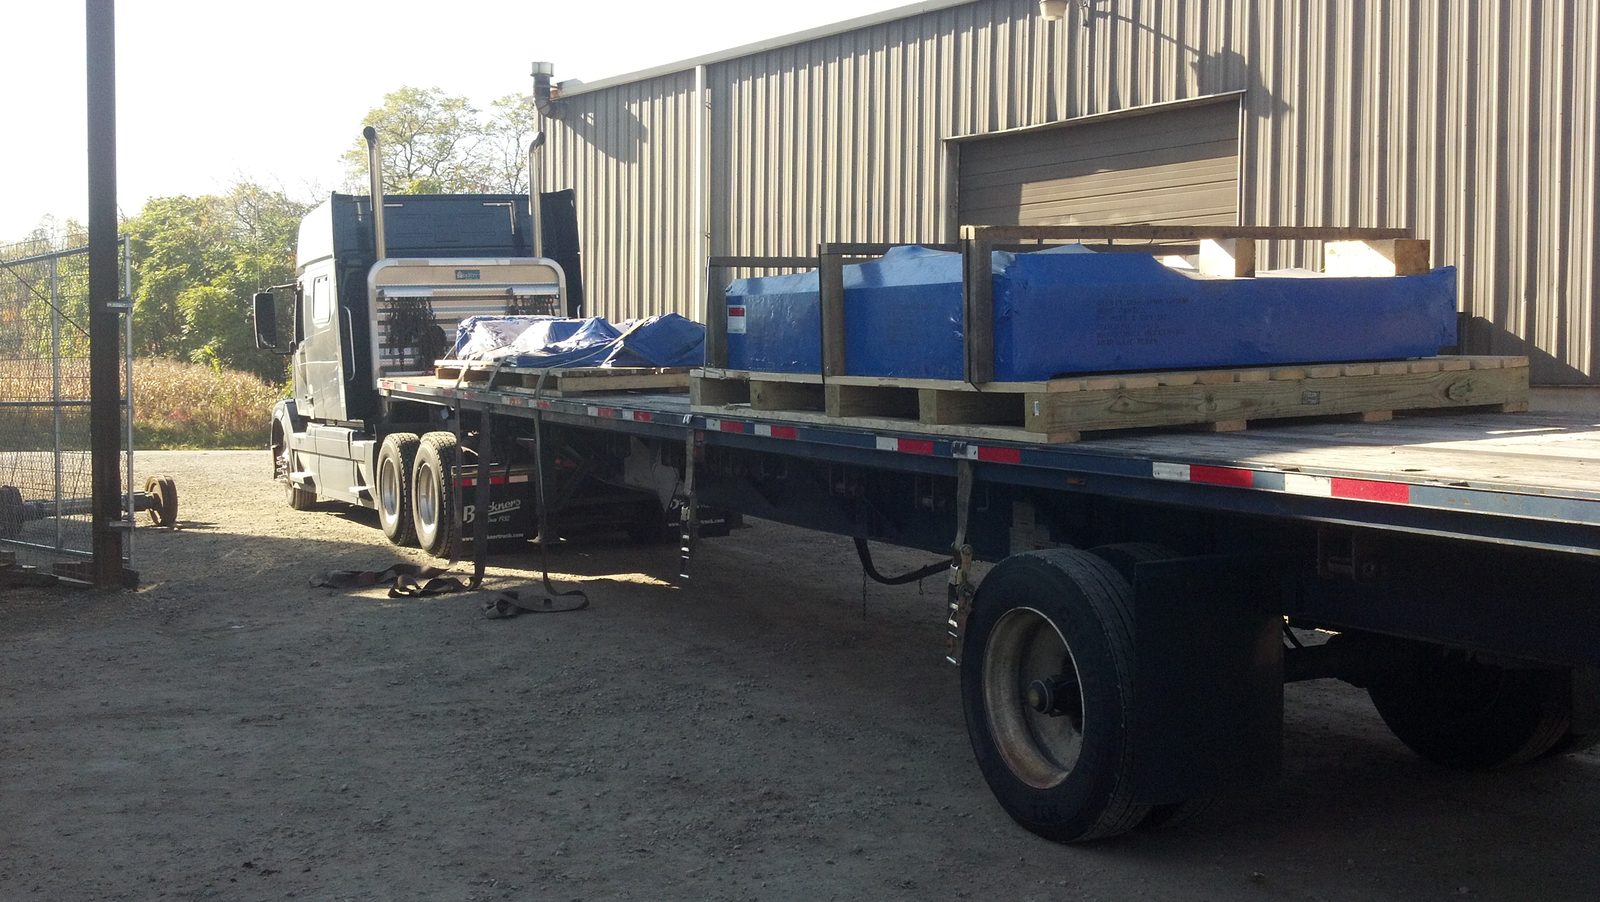
- Coated parts crated and shipped from the same building
- Galvanizing, plating, and specialty coating systems handled through qualified outside suppliers when a specification calls for them
The Last Operation, Not a Separate Vendor
Blasting and coating are how a Westmoreland Steel job finishes. They are part of the turnkey scope — cut, formed, welded, machined, inspected, coated, and crated on one purchase order with one point of accountability.
Typically Coated Here
- Compressor bedplates and skid bases
- Structural mounting bases and frames
- Bins, hoppers, chutes, and tanks
- Walkways, stairs, ladders, and platforms
Then It Ships
- Custom crating for domestic and international shipment
- Coordinated through specialty trucking partners
- Inspection documentation with the shipment
- Compliance and certifications
Equipment and capacities are current as of the date shown and are subject to change. Contact us to confirm capability, capacity, and tolerance for a specific part or program.
Have a Coating Specification?
Send the drawings and the coating callout together. We will confirm the prep grade, the system, and what gets documented before the job is released — and quote the fabrication and the finish as one number.
Request a Quote All Processing Capabilities